Selection
Technical Insights
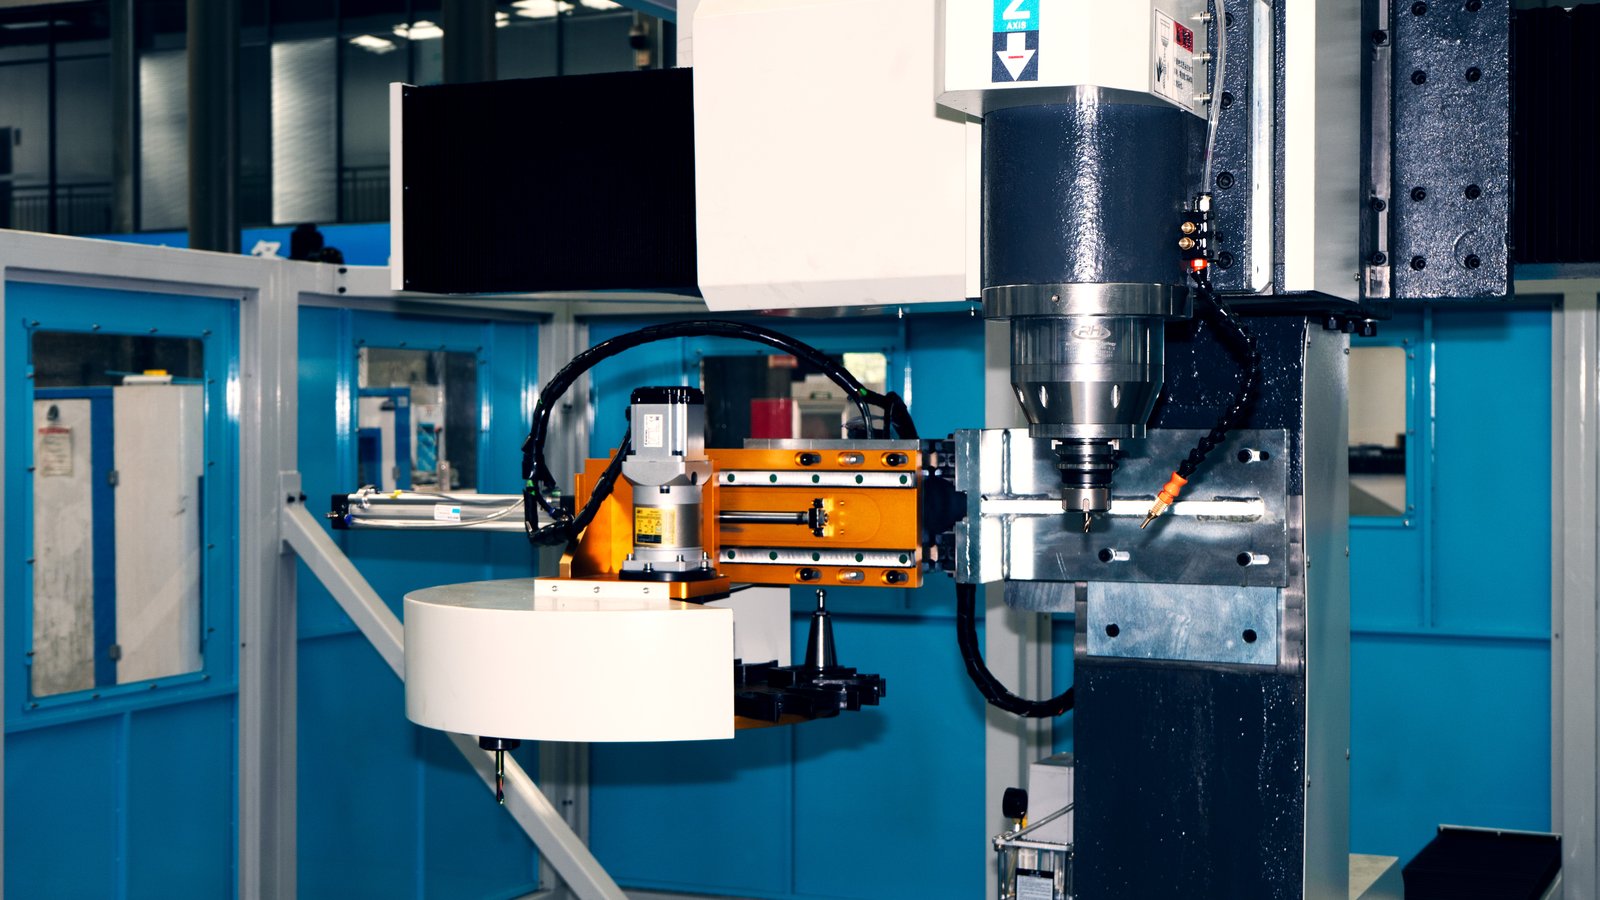
EV battery trays, sill beams and bumper beams share a profile: long workpieces, thin walls, dense hole patterns and tight tolerances. A single tray can carry several hundred holes — module mounting holes, cold plate ports, lifting points, grounding points — while the flatness of the sealing face directly determines the ingress protection rating of the pack. The most common failure with this kind of work is not that the part cannot be made; it is dimensional drift caused by clamping distortion and thermal growth.
1. Rigidity for long workpieces: bed first, then support
When machining long parts, cutting force deflects the workpiece, and once the clamps are released the part springs back — this is exactly why a part that measures good on the machine goes out of tolerance on the bench.
- Prefer a one-piece cast bed, or a welded structure that has been annealed to relieve stress; look at bed weight relative to span
- Distribute table support points evenly along the workpiece length, avoid an unsupported middle
- For thin-wall parts use multi-point support or contoured fixtures to spread the clamping force
- At acceptance require an actual cutting test at full stroke, not just a static accuracy check
2. Clamping: never clamp a thin-wall part on one side
Two hard rules for thin-wall profiles: do not clamp a long workpiece on one side only (it will bend), and keep the clamping force perpendicular to the support surface (an angled component will push the profile out of position).
- Prefer pneumatic or hydraulic fixtures so clamping force is repeatable every cycle
- Separate the locating face from the clamping face so the datum is not dragged by clamping force
- Aluminium is poorly magnetic; check suitability before considering magnetic fixtures
- For high-changeover lines choose modular fixtures with locating pins to cut alignment time
3. Spindle torque matters more than top speed
Aluminium machining is often oversold on "high rpm". What really sets metal removal rate is torque across the usable speed band. Heavy roughing needs torque reserve at low rpm, and tapping is the clearest case: a spindle rated at 30,000rpm that lacks torque when tapping above M10 will break taps routinely.
- Read the torque curve, not just peak speed and peak power
- Check the duty rating (S1 continuous / S6 intermittent); continuous work needs sustained output
- For heavy depths of cut choose BT40 or larger tapers for rigidity headroom
- Ask the builder for cutting videos and tool-life data on the same material and cutter diameter
4. Chip evacuation: the hidden bottleneck for thin-wall work
Battery trays carry dense hole patterns. Chips that cannot get out wrap around the cutter, scratch finished surfaces and break tools — and this shows up most in deep and blind holes.
- Prefer a slanted bed or steep chip fall geometry to reduce chip retention
- Confirm the cooling method: mist or minimum quantity lubrication controls thermal distortion better on thin walls
- Use through-tool coolant with a pecking cycle for deep holes
- Verify chip conveyor service access before purchase; many lines cannot be retrofitted later
5. Work out the cycle time before choosing the configuration
For large parts like battery trays, cycle time is usually set not by cutting time but by tool changes multiplied by change time, plus table travel. Before ordering, have the builder run a full calculation against your hole list:
- Hole count per part and number of diameters
- Estimated tool changes and time per change
- Number of full-stroke table traverses
- Loading method and time
- Tool life and replacement frequency
Typical battery tray operations and the matching WGTB-6500 configuration
| Operation | Processing challenge | Matching WGTB-6500 specification |
|---|---|---|
| Drilling module mounting and cold-plate port holes | Dense hole patterns; chips wrap around the tool | BT40 direct-drive spindle · 7.5 kW · 12,000 rpm with automatic chip conveyor |
| Sealing face milling | Flatness determines the ingress-protection rating of the pack | Positioning accuracy X ±0.05 / Y ±0.02 / Z ±0.02 mm, repeatability ±0.02 mm |
| Tapping lifting and earthing threads | High torque at low speed; insufficient torque breaks taps | Rated torque 52.5 N·m, no speed increaser required |
| Single-setup machining of beams up to 6.5 m | Deflection under cutting load, spring-back after unclamping | 6500 × 650 mm table with five T-slots for zoned clamping |
| Changeovers across many part variants | Many hole sizes mean frequent tool changes | 24-pocket arm-type magazine, 1.8 s tool-to-tool |
| Loading and support of heavy workpieces | Impact during crane loading, unstable support affects dimensions | Maximum table load 5000 kg with zoned support stands |
FAQ
- BT30 or BT40 for battery tray work?
- BT30 is sufficient when the work is mainly thin-wall aluminium and depths of cut stay modest. Choose BT40 when heavy roughing, steel insert machining, or a larger rigidity margin is involved.
- How do you control distortion when machining thin walls?
- Three directions: switch to multi-point support with contoured clamping to spread the clamping force; use a symmetric machining sequence so stress releases evenly; and use mist cooling to cut heat input. Leaving time between roughing and finishing for stress to relax also matters.
- Does accuracy decay on long-stroke machines?
- Yes, mainly from guideway and ballscrew wear. Specify a linear scale for closed-loop control and set up quarterly accuracy verification — correct it as soon as error exceeds 0.05mm.
Parts like battery trays make heavy demands on rigidity, chip evacuation and cycle time. Send us the part drawing and your output target, and we will come back with a specific configuration and a trial cutting schedule.